
Eighteen Million Stainless Spring Clips a Year for Door Hardware
Table of Contents
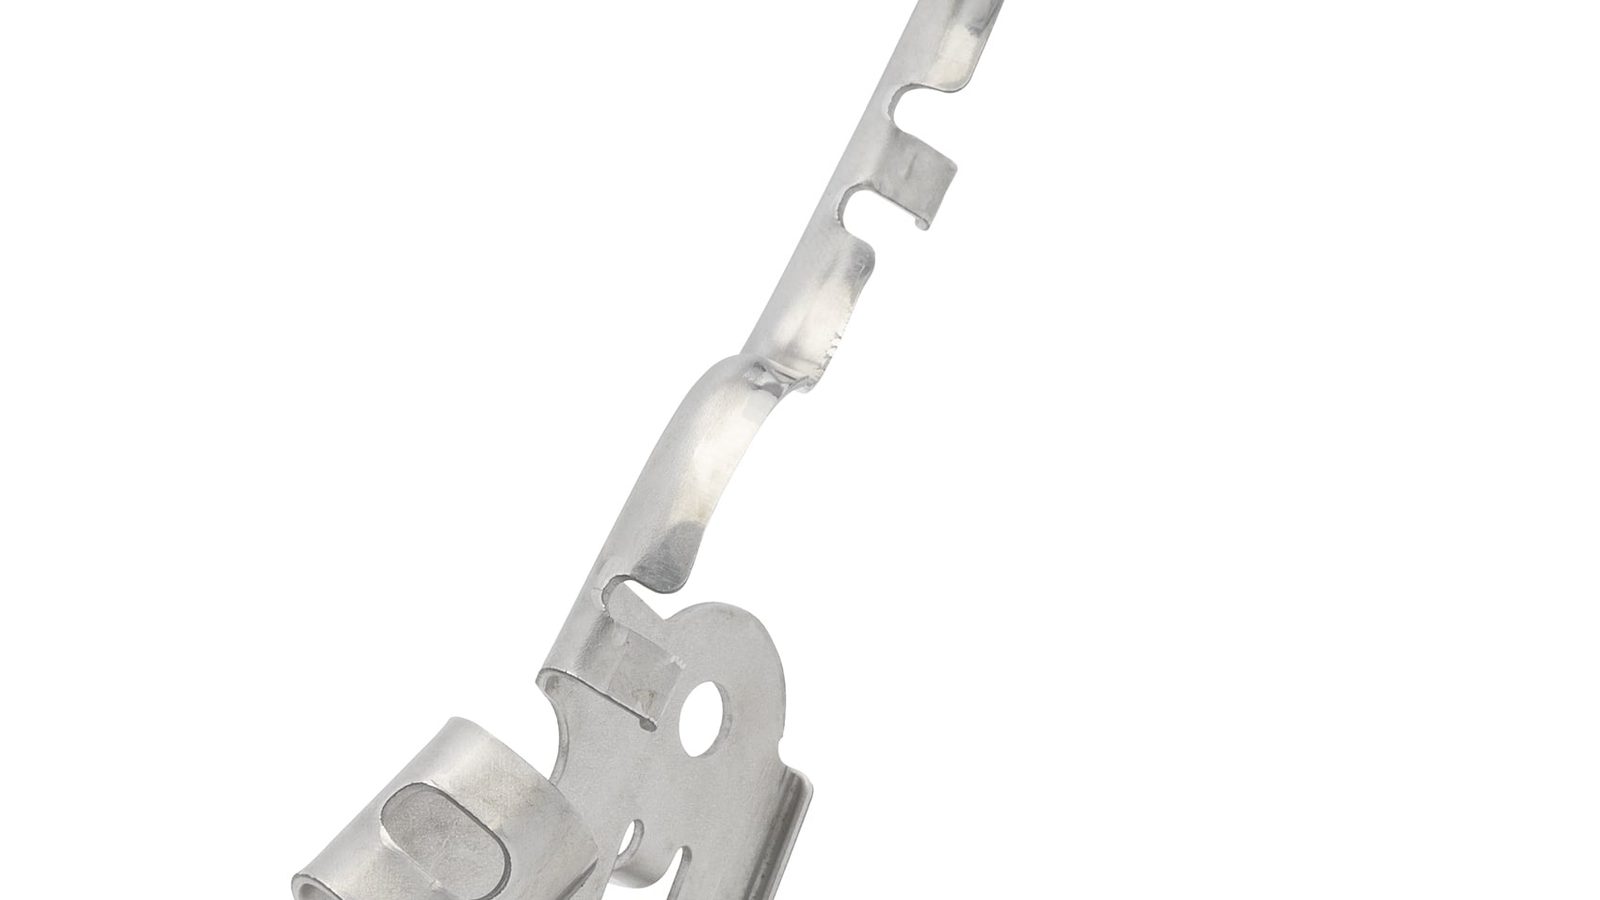
A door-hardware brand running multi-country assembly plants was qualifying a second source for a long stainless spring clip. The incumbent part bowled out of spec after 200,000 cycles because the forming step was being corrected by hand at the press.
We designed and built the progressive die in-house with a coining station that sets the radius directly in the tool, so springback stops being an operator variable. Material #301 stainless, 0.6 mm gauge, full round-edge stock to protect the mating surface.
Outcome
- 18,000,000 clips per year across weekly releases of 275,000
- Tightest tolerance ±0.005 mm; 125 mm overall length held consistently on formed stainless
- No hand correction stations on the line — forming parameters live in the die
- Customer audits incoming on their own vision system; PPAP-style documentation supplied
Specifications
SUS301 · 0.6 mm · progressive die + coining · 25–110 T press range · tooling lead 2–5 weeks · MOQ 10,000
Industries Served
See how we stamp for ApplianceMore Case Studies
NEXT STEP
Have a Similar Part?
Send your drawing and annual volume — our engineers return a DFM review and quote for parts like this one.
Written by
Ray ChanExport Brand Manager. Ray helps global engineers and buyers source precision metal stamping parts and assemblies.